Butt fusion welding table for HDPE pipes
2023-07-06
Read more
Ziyolilar street, 4 a Tashkent, Uzbekistan
|
Working hours: Mon-Sun 9:00 - 18:00
Why HDPE pipe joints leak and how to prevent it: end preparation, clamping, SDR, heating and cooling time, joining pressure.
2023-07-06
An HDPE pipe joint usually leaks because of poor preparation, and only then because of the machine. An oxide layer left on the pipe, grease on the end, misaligned pipes, an uneven facing cut, a coupler that sits off its marks and pipes of different SDR spoil the joint before the heater is even switched on. During welding itself, the typical mistakes are wrong heating time, short cooling time and wrong joining pressure. For each mistake we give a way to avoid it in butt fusion and electrofusion welding.
The tightness and strength of the joint depend on preparation. A welder spends more time on this stage than on heating, and this is where people most often cut corners.
Polyethylene oxidises in air, and the outer layer of the pipe becomes harder to melt. In electrofusion welding this layer does not fuse with the coupler, which leaves a local lack of fusion. At pressures from 6 bar such a joint is the first to leak.
The layer is removed with a mechanical scraper: a hand scraper suits pipes of 16-200 mm, and for larger diameters rotary tools are used that take off the shaving without turning the pipe. The scraped length should equal the insertion depth into the coupler plus 5-10 mm. Sandpaper is not suitable: the abrasive gets embedded in the polyethylene and interferes with fusion.
After transport and unloading, pipes carry sand, dust and traces of technical fluids. These inclusions prevent the polyethylene from fusing at the molecular level, and the weld becomes porous. For butt fusion, wipe the pipe end and 20 mm of surface around it. For electrofusion, clean the whole zone that goes inside the fitting, with some margin. Lint-free wipes with alcohol work well. Solvents that leave a film on the surface are not suitable.
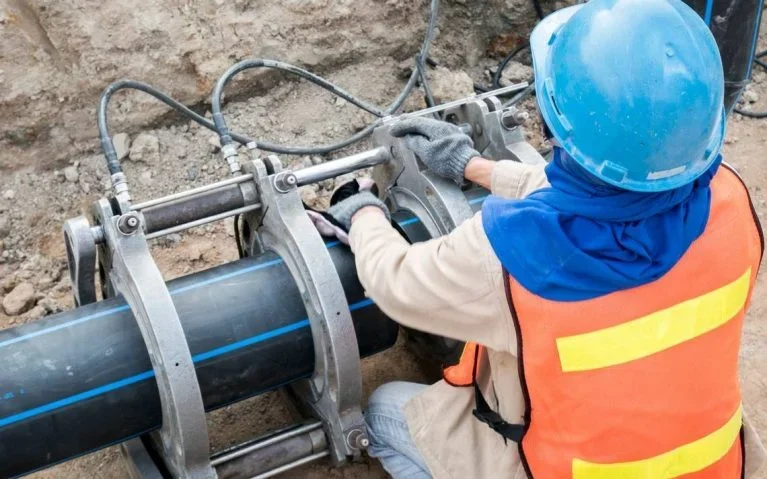
If the pipes lie on the ground without supports and clamps, they shift during heating and joining. In butt fusion, alignment is set by the machine's clamps with inserts for the diameter, which hold both pipes on one axis. The permissible edge misalignment is no more than 10% of the wall thickness. In electrofusion, positioners are used: strap clamps for large diameters and threaded metal clamps for small ones. Without them the coupler is welded at an angle, and the pipeline gets a bending stress right in the weld zone.
A saw, angle grinder or jigsaw does not give a straight cut. When the ends are brought together, even with melting of up to 5 mm, gaps remain on an uneven edge and later turn into pinhole leaks. Before butt fusion the ends are machined with the facing tool of the machine for that diameter until a continuous ribbon of shaving comes off both pipes. After facing, the ends are brought together and the gap is checked: for pipes up to 355 mm it must not exceed 0.5 mm.
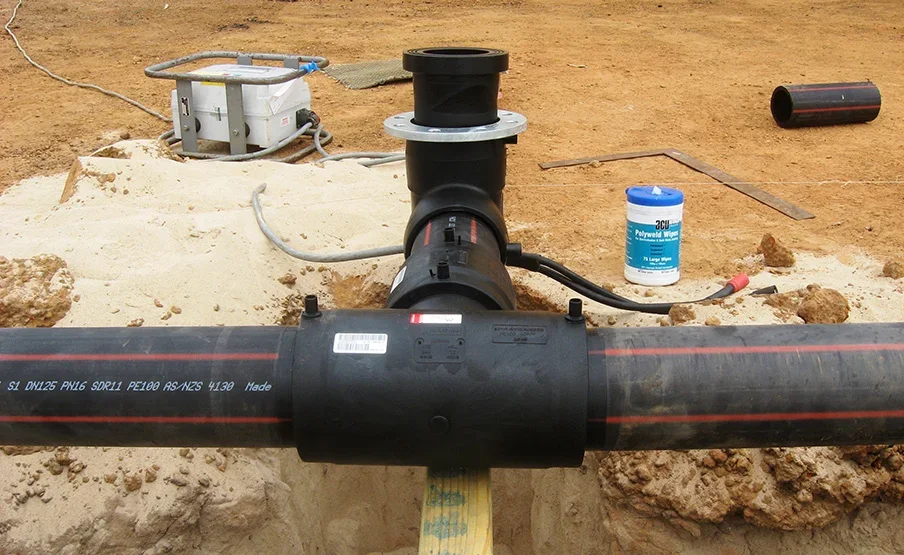
Some fittings have an internal stop, and the pipe just needs to be pushed in fully. In couplers without a stop, a common mistake is that one pipe goes in deep and the other only 20-30 mm. The fusion area on the short side is small, and the joint holds worse. To avoid this, measure the coupler with a tape, divide the length in half and mark both pipes with a light-coloured marker. Start welding when both marks sit at the edges of the coupler. This matters most for repair inserts, where the coupler is first slid fully onto one end and then moved back onto the mating pipe.
SDR is the ratio of the outside diameter to the wall thickness. Two 110 mm pipes can have a wall of 6.6 mm (SDR 17) or 10 mm (SDR 11). Butt welding them properly is impossible: ends of different thickness heat unevenly. Moulded fittings are also matched to the SDR of the pipe. Before buying, compare the markings on the pipe and the fitting, and for butt fusion use fittings of the same SDR as the pipe.
Welding parameters depend on the diameter and wall thickness, so they are taken from the machine's table and never set by eye.
If heating is too short, the polyethylene does not melt deep enough, and the ends merely stick together. Such a weld can pass the hydraulic test and fail months later. If heating is too long, the melt runs out, the ends deform and the bead becomes too large. Heat soak time depends on the wall: roughly 10 seconds per millimetre. Full parameters are collected in the article butt fusion welding table for HDPE pipes.
While the weld is hot, it cannot carry a load. Electrofusion units read the cooling time from the fitting's barcode, but in butt fusion it is entered by hand, and mistakes are easy. Removing the pipe from the clamps too early or moving it creates internal stresses in the weld. For a pipe with a 10 mm wall, cooling under pressure takes about 14 minutes, with a 30 mm wall about 37 minutes.
In butt fusion, the pressure on the pipe ends is calculated from the area of the pipe end and the cylinder area of the machine, plus the drag pressure needed to move the carriage. Too little pressure gives a weak weld. Too much pressure squeezes the melt out of the joint, the bead becomes huge and the pipe shortens more than planned, so it may not reach the connection point.
The Russian code SP 42-103-2003 allows welding polyethylene pipes at air temperatures from -15 to +45 °C. Outside this range, work is done only in a tent or shelter. Wind cools the heater plate and the pipe ends, so the open ends of the pipe are closed with caps to stop draughts from drawing heat out. In direct sun one side of the pipe gets hotter than the other, which also changes heating.
A butt weld is checked by its bead. It must be double, even around the whole circumference, without pores or cracks, and the groove between the two halves of the bead must not drop below the pipe surface. The width and height of the bead depend on the wall thickness, and differences around the circumference indicate uneven heating or misalignment.
For an electrofusion joint, look at the fusion indicators on the fitting: they must pop out. Melt must not run out from under the edge of the coupler, and the marks on the pipes must stay at its edges. Modern machines save a record of each joint: time, temperature, voltage. On gas pipelines this record is attached to the as-built documentation.
| Stage | What to check | What a mistake leads to |
|---|---|---|
| Preparation | Oxide layer removed, ends degreased | Lack of fusion and leaks under pressure |
| Assembly | Alignment, edge offset no more than 10% of wall | Stress in the weld, crooked pipeline |
| Facing | Continuous shaving, gap no more than 0.5 mm | Pinhole leaks at the joint |
| Parts selection | Same SDR for pipe and fitting | Uneven heating, weak weld |
| Welding | Heating time, joining pressure and cooling time per table | Cold weld or squeezed-out melt |
| Inspection | Bead shape or coupler indicators, machine record | Defects that appear after backfilling |
Most of these mistakes are prevented by the right equipment: a butt fusion machine with clamps and a facing tool for the diameter, and an electrofusion unit that reads the mode from the fitting. Polimer Group Asia supplies butt fusion machines for pipes up to 1600 mm with warranty and service, as well as electrofusion fittings for PE100 pipes. The company's specialists train welders.
The plant has a capacity of 10,000 tons of polyethylene pipes per year. Our specialists carry out design and survey, design work on installation, installation and laying of pipelines for hot and cold water supply, heating, sewage, heating mains and drainage systems.
Address
Ziyolilar street, 4 a Tashkent, Uzbekistan